Stick welding can look simple: clamp the ground, strike an arc, and move the rod. Good results take more care. These 10 practical tips focus on the choices that shape strong, consistent Stick Welding Welds, from selecting an electrode to controlling travel speed. Small changes matter. A rod held at the wrong angle can leave a rough bead, while an unstable arc may cause sticking, spatter, or uneven fusion. Clean metal, suitable amperage, and a steady hand provide a better starting point. The workpiece and welding position also affect the result.
The guidance covers common shop practices and details welders check at the bench: electrode condition, joint preparation, arc length, and slag removal between passes. Follow the electrode maker’s instructions and your welding machine’s guidance; no single amperage or technique suits every job. Wear appropriate protective gear, secure the work, and keep the area clear of flammable materials. Safety is part of weld quality. A sound-looking bead does not prove sound fusion, so inspect the joint and practice on scrap before tackling important work. I still find that a rushed pass can look acceptable at first, then reveal uneven edges after cleaning. That is worth remembering. These tips offer a practical starting point, not a substitute for qualified instruction or inspection when a weld is safety-critical. Make each pass more controlled, notice what went wrong, and improve the next one.
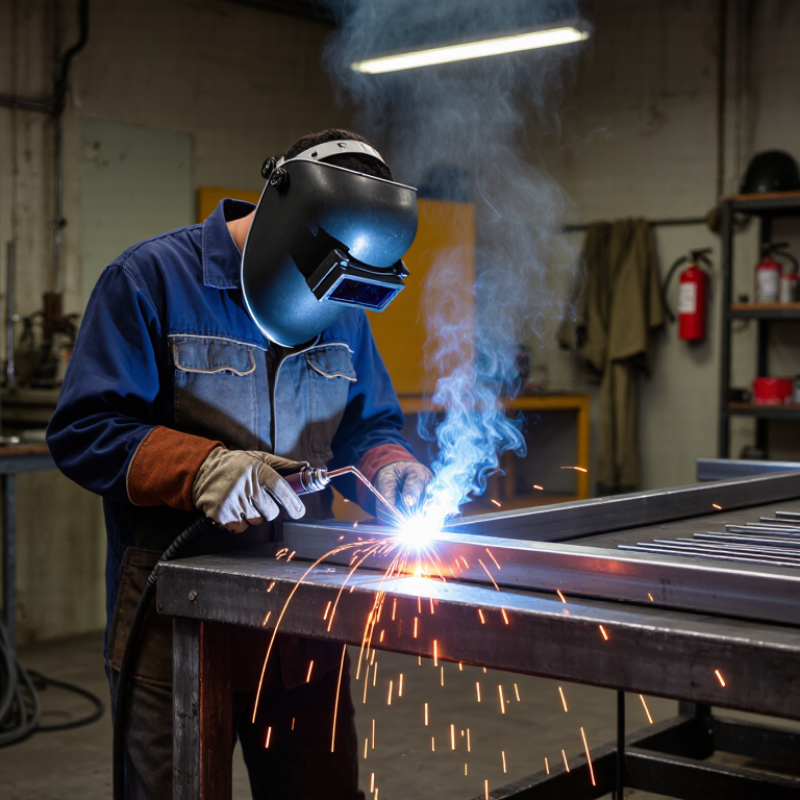
A steady arc cannot compensate for a dirty or poorly prepared joint. Remove paint, rust, oil, and moisture from the welding area, extending a little beyond the bead path. A wire brush may clear loose scale, but stubborn coatings need more careful removal. Check the workpiece edges and fit-up; uneven gaps can make a beginner chase the puddle instead of controlling it. Keep the metal dry, and follow safe handling practices around sparks and hot surfaces.
Tip: Before striking an arc, wipe the joint and inspect it under good light. Look for grease near corners and damp spots after the metal has been stored outside. Clamp the pieces so they cannot shift. I sometimes overlook a thin coating near an edge; it can still cause spatter or a rough bead. Preparation takes a few extra minutes, but rushing it often costs more time later.
Tip: Choose an electrode suited to the base metal, joint position, and available current. Check its label and the equipment guidance rather than guessing from color or size alone. Keep electrodes dry and store them as their instructions specify; moisture can affect arc behavior and weld quality. For a first pass, test the settings on clean scrap of similar thickness. The scrap may not match perfectly, so treat the result as a useful check, not a guarantee.
Prepare the Workpiece and Choose the Right Electrode
These are typical amperage starting ranges; actual recommendations vary by electrode and welding conditions. Clean the workpiece to bare metal near the joint, then check the electrode packaging and adjust for position, polarity, and material thickness.
Set current from the electrode diameter, metal thickness, joint position, and polarity—not from habit. AWS A5.1/A5.1M:2021 classifies E7018 as a 70-ksi minimum-tensile-strength electrode; its “1” indicates all-position use. That strength code does not specify amperage. Check the electrode package or technical data sheet for its operating range, then start near the middle. For a 1/8-inch rod on mild steel, a common starting window is roughly 110–140 amps, subject to the electrode’s instructions. Too little current makes the rod stick and leaves a tall bead. Too much can undercut the plate or flatten the bead.
Match the rod to the steel and the work. A thin sheet needs lower heat and a smaller electrode; a thick joint may need more current or multiple passes. On a scrap coupon of similar thickness, strike an arc and listen: steady crackle is useful, while frequent sticking or a harsh, wandering arc suggests adjustment. Confirm polarity before welding; many E7018 electrodes run on DCEP, but the product data sheet controls. Small details matter. Keep the rod angle consistent, and watch the puddle’s edges, not just the bright center. I still find that a setting that looks right on the dial can behave differently on a cold, rusty plate. Clean the test area and make one adjustment at a time.
A clean start begins with a controlled strike, not a hard jab. Scratch the electrode briefly, then lift it just enough to establish the arc. The American Welding Society’s Welding Handbook identifies arc length as a key factor in arc voltage and weld-bead control. A useful shop rule is to keep the arc close to the electrode’s core diameter. With a 1/8-inch rod, aim for roughly a 1/8-inch gap. Too long, and the arc may hiss, wander, and throw spatter. Too short, and the rod can stick. It happens.
Watch the puddle, not just the electrode tip. Hold a steady travel speed and keep the rod angle consistent; small changes can leave a bead that is wide in one spot and narrow in another. If the arc sputters, pause your hand and check the gap before changing several settings at once. That makes the cause easier to spot. AWS welding guidance treats current, travel speed, and arc length as connected operating variables, so adjust one at a time when possible. A slight tremor is normal, even for experienced welders. Still, uneven beads deserve a second look. Use a welding helmet and suitable protective clothing; OSHA warns that arc rays can injure eyes and burn skin.
Stick welding rewards steady movement more than speed. Keep a short, consistent arc, and hold the electrode at a slight angle in the direction of travel, usually around 5 to 15 degrees. The exact angle depends on the electrode, joint, and welding position. Tip: Watch the puddle, not just the rod. It should stay visible and move evenly along the joint. If it races ahead, slow down; if it piles up, check your speed and arc length. Small changes matter.
Travel speed shapes the bead. Moving too quickly can leave a narrow bead with poor tie-in at the edges. Moving too slowly may create a wide, lumpy bead and excess heat. Aim for a uniform width, and pause briefly at each edge if the joint needs better coverage. Not too long. A simple test is to weld a short bead on scrap of similar thickness, then inspect its profile after it cools. Slag can hide flaws, so remove it before judging the result.
Tip: Compare your bead with the joint edges. A consistent bead should blend into both sides without obvious gaps or tall ridges. If it wanders, reduce your travel distance and focus on a fixed point just ahead of the puddle. Be honest about the result: a neat surface does not prove strong fusion. Adjust one variable at a time, and note what changes. Some beads will still look uneven; that is useful feedback, not a reason to keep the same settings blindly.
| 10 Stick Welding Tips for Better Welds - Control Travel Speed, Angle, and Weld Bead | |||
|---|---|---|---|
| No. | Welding Factor | Practical Tip | What to Look For |
| 1 | Joint preparation | Remove rust, paint, oil, moisture, and loose scale from the weld area. For thicker material, prepare the joint and root opening to suit the joint design and welding procedure. | Clean, accessible surfaces and a consistent fit-up help reduce contamination and lack of fusion. |
| 2 | Electrode selection | Choose an electrode suited to the base metal, joint, position, and required properties. Check its packaging or procedure for permitted current type, polarity, and amperage range. | The electrode should run steadily and deposit weld metal appropriate for the joint and position. |
| 3 | Amperage | Set current within the electrode manufacturer's recommended range, then make a test weld on similar material. Adjust for electrode diameter, position, joint, and how the arc behaves. | Too little current can cause a sluggish arc and poor fusion; too much can cause excessive spatter, undercut, or an overly fluid puddle. |
| 4 | Arc length | Keep a short, steady arc, generally close to the electrode core-wire diameter, while following the electrode's operating guidance. Avoid letting the electrode touch the puddle continuously. | A consistent arc helps control spatter and bead shape; an excessively long arc can make the arc unstable and increase porosity risk. |
| 5 | Travel angle | For many flat-position stick welds, use a slight drag angle, often about 5–15 degrees from perpendicular in the direction of travel. Follow the electrode guidance and adjust for the position and joint. | A controlled angle helps direct the arc and slag behind the puddle without pushing slag ahead of the weld. |
| 6 | Work angle | Aim the electrode toward the joint. A butt joint often starts near a 90-degree work angle; an equal-leg T-joint fillet often starts near 45 degrees. Adjust as needed for unequal thicknesses and welding position. | The arc should reach both joint faces so the weld fuses evenly rather than favoring one side. |
| 7 | Travel speed | Move at a steady pace and watch the puddle rather than the electrode tip alone. Slow down if the bead is narrow or fusion appears insufficient; speed up if the bead becomes overly wide or the puddle runs ahead. | A consistent bead width and smooth tie-in along both edges are useful visual cues. |
| 8 | Bead control | Use a straight stringer bead for many applications. If a weave is needed, keep it controlled and within the limits of the welding procedure; pause briefly at the toes when appropriate. | Look for a reasonably uniform profile, smooth transitions at the toes, and no visible undercut or overlap. |
| 9 | Starts and stops | Strike the arc in the weld area or on a run-on tab when available. At a restart, remove slag, strike ahead of the crater, and move back into it before continuing. | Filling the crater and blending the restart helps reduce crater defects and discontinuities. |
| 10 | Slag and inspection | Let the weld cool enough for safe handling, then remove slag between passes and inspect the bead before welding over it. Wear suitable eye, skin, and respiratory protection and keep the work area fire-safe. | A clean pass makes defects easier to spot and helps prevent slag inclusions in subsequent passes. |
After the weld cools enough to inspect safely, remove the slag with a chipping hammer and wire brush. Wear eye protection; small chips can travel farther than expected. Brush along the bead, then check both edges where the weld meets the base metal. A clean surface makes flaws easier to see.
Look for a fairly even bead, consistent width, and smooth tie-in at the edges. Pinholes, visible cracks, deep undercut, or missed spots deserve attention. So do abrupt starts and stops. I once focused too much on the bead’s appearance and missed a shallow groove along one edge. It looked tidy from above. It was not a detail to ignore. Don’t grind over a suspected defect just to make the surface look smooth; confirm what it is and follow the applicable welding procedure before repair.
Use good light and view the weld from more than one angle. A small mirror can help in tight areas. Compare the result with the job requirements, since a sound-looking bead alone does not prove the joint is acceptable. If the inspection is uncertain, pause and ask a qualified welding inspector or supervisor. That pause can feel fussy. It is still better than guessing.